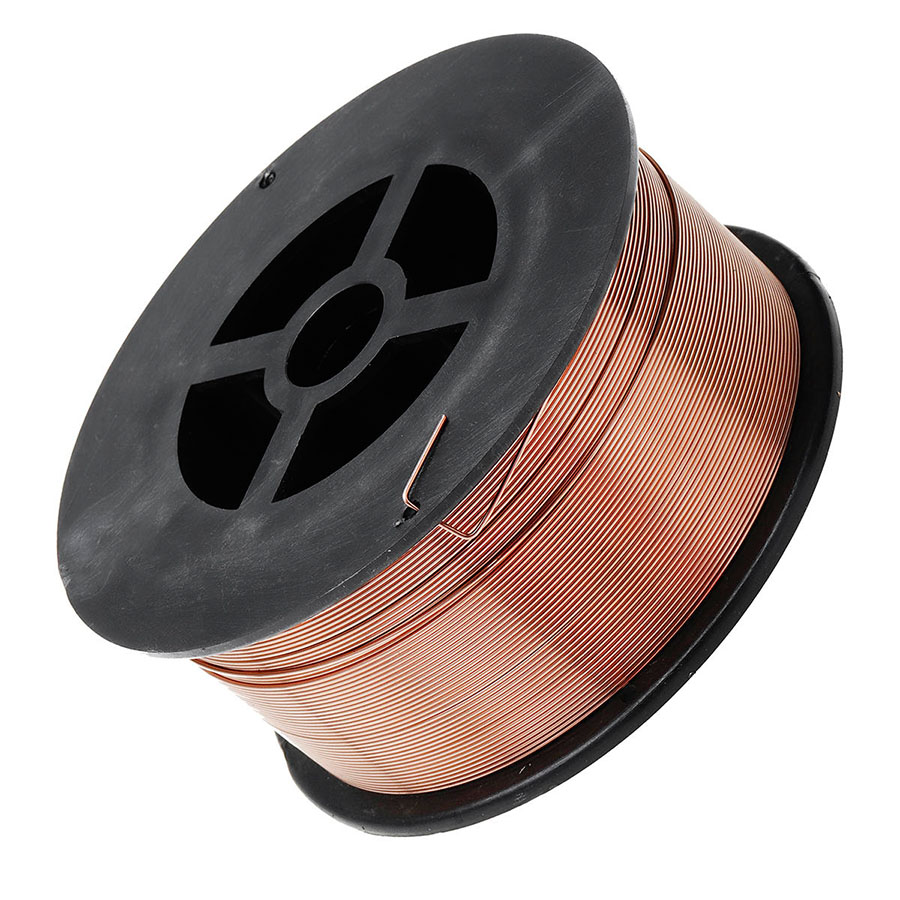
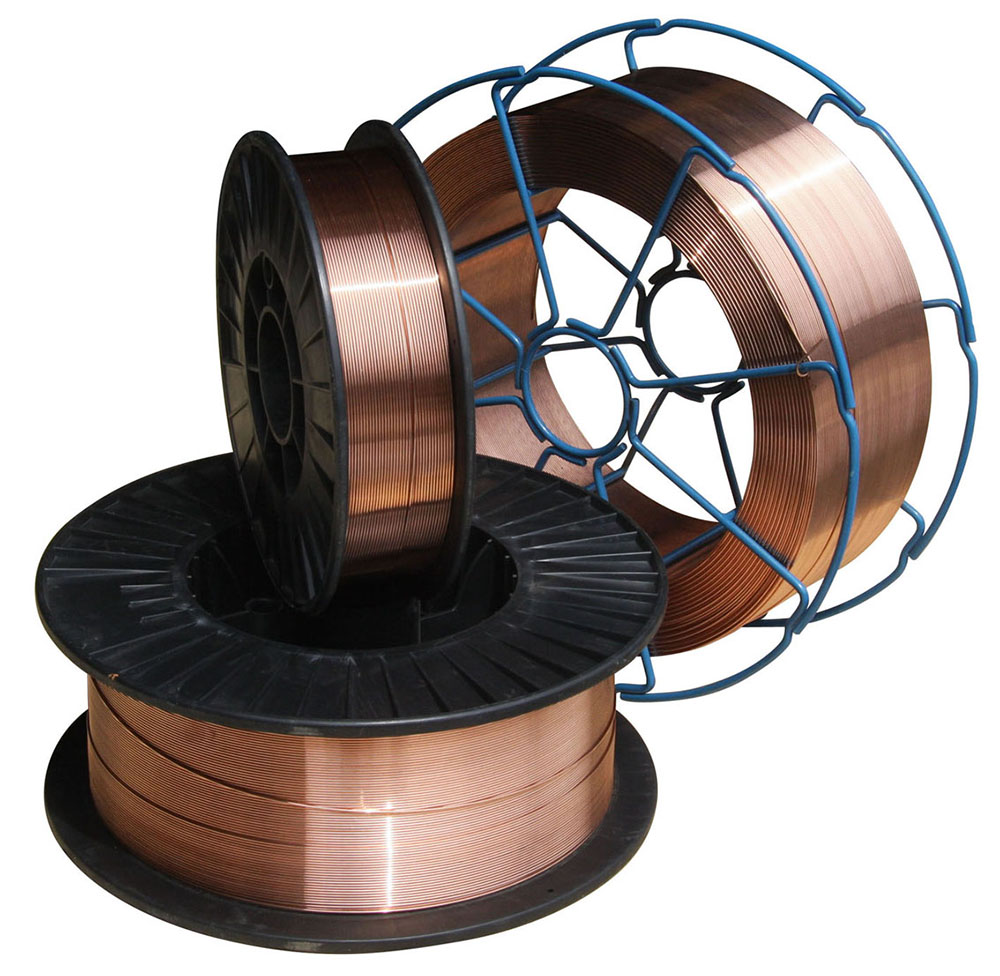
KYA ER70S-6 CO2 Welding Wire 1.0mm is a copper-coated mild steel solid welding wire designed for gas metal arc welding (GMAW/MIG/MAG). It is suitable for welding carbon steel and selected low-alloy steel components using 100% CO2 or argon-CO2 mixed shielding gas.
The ER70S-6 wire classification contains manganese and silicon deoxidizers that help support weld quality when working with properly prepared steel surfaces. The wire is intended to provide stable feeding, consistent arc performance and well-formed weld beads under suitable welding conditions.
With a nominal wire diameter of 1.0mm, this product can be considered for structural steel fabrication, machinery manufacturing, shipbuilding and other industrial welding operations where ER70S-6 filler metal is specified.
Copper-Coated Solid Wire: Designed for gas-shielded MIG/MAG welding of carbon steel.
1.0mm Wire Diameter: Suitable for welding equipment configured for 1.0mm solid wire.
Stable Wire Feeding: Supports consistent wire delivery when used with suitable drive rolls, liners and contact tips.
Arc Performance: Designed for stable arc operation and consistent weld bead formation under appropriate welding parameters.
Deoxidizing Elements: Manganese and silicon contribute to deoxidation during welding.
Shielding Gas Options: Suitable for 100% CO2 and compatible argon-CO2 shielding gas mixtures.
All-Position Welding: Can be used in different welding positions when the welding procedure and metal transfer mode are appropriate.
Industrial Applications: Intended for carbon steel fabrication, steel structures, machinery and selected low-alloy steel components.
The following product information covers the KYA 1.0mm ER70S-6 welding wire, its classification, shielding gas options and published packaging arrangements.
| Product Name | CO2 Welding Wire 1.0mm |
|---|---|
| Brand | KYA |
| Product Code | KYA-ER70S-6/1.0MM |
| AWS Classification | ER70S-6 |
| GB Classification | ER50-6 |
| Wire Diameter | 1.0mm |
| Wire Type | Copper-coated solid welding wire |
| Welding Process | GMAW / MIG / MAG |
| Shielding Gas | 100% CO2 or argon-CO2 mixed gas |
| Welding Positions | All positions, subject to welding procedure and transfer mode |
| Published Weight Options | 5kg, 15kg, 20kg |
| Published Packaging | 15kg/D270 plastic spool; 16kg/box |
| Pallet Packing | 72 boxes/pallet |
| Container Loading | 24 pallets/1 x 20' GP |
| Payment Terms | 30% T/T in advance, 70% balance against B/L copy |
| Published Lead Time | 10–25 days after receipt of deposit |
For bulk purchasing, customers can specify their required wire diameter, spool weight, shielding gas application and shipment quantity when requesting a quotation. Final packing and delivery arrangements should be confirmed with KYA.
ER70S-6 is a carbon steel solid welding wire classification containing manganese and silicon deoxidizers. The following ER50-6 / ER70S-6 composition values are listed in the original KYA product comparison data.
| Element | ER50-6 / ER70S-6 Composition (%) |
|---|---|
| Carbon (C) | 0.06–0.15 |
| Manganese (Mn) | 1.40–1.85 |
| Silicon (Si) | 0.80–1.15 |
| Phosphorus (P) | ≤0.025 |
| Sulfur (S) | ≤0.035 |
| Copper (Cu) | ≤0.50 |
The chemical composition of an individual production batch should be checked against the applicable product documentation when specific material requirements apply.
The original KYA comparison table lists the following mechanical properties for the ER50-6 / ER70S-6 classification.
| Mechanical Property | Source-Listed Value |
|---|---|
| Yield Strength (σs) | ≥420 MPa |
| Tensile Strength (σb) | ≥500 MPa |
| Elongation (σ5) | ≥22% |
| Impact Energy (AKV) | ≥27 J at -29°C |
These values are reproduced from the published product comparison data and should not be interpreted as batch-specific test results. Actual deposited weld metal properties depend on the welding procedure, shielding gas, joint conditions and testing requirements.
Different welding wire classifications have different chemical compositions, mechanical property requirements and application characteristics. The following comparison retains the grade information supplied in the original KYA product description.
| Property | ER49-1 | ER50-3 | ER50-4 | ER50-6 | ER50-G |
|---|---|---|---|---|---|
| Classification | GB: ER49-1 AWS: – | GB: ER50-3 AWS: ER70S-3 | GB: ER50-4 AWS: ER70S-4 | GB: ER50-6 AWS: ER70S-6 | GB: ER50-G AWS: ER70S-G |
| Size (mm) | 0.9–1.6 | 0.8–1.6 | 0.8–1.6 | 0.8–1.6 | 0.8–1.6 |
| Chemical Composition (%) | C: ≤0.11 Mn: 1.8–2.1 Si: 0.65–0.95 P: ≤0.030 S: ≤0.030 Cr: ≤0.20 Ni: ≤0.30 Cu: ≤0.50 | C: 0.06–0.15 Mn: 0.9–1.4 Si: 0.45–0.75 P: ≤0.025 S: ≤0.035 Cu: ≤0.50 | C: 0.07–0.15 Mn: 1.00–1.50 Si: 0.65–0.85 P: ≤0.025 S: ≤0.035 Cu: ≤0.50 | C: 0.06–0.15 Mn: 1.40–1.85 Si: 0.80–1.15 P: ≤0.025 S: ≤0.035 Cu: ≤0.50 | C: ≤0.10 Mn: 1.40–1.90 Si: 0.55–1.10 P: ≤0.030 S: ≤0.030 Al: ≤0.10 Ti: 0.12–0.20 Cu: ≤0.50 |
| Mechanical Properties | σs: ≥372 MPa σb: ≥490 MPa σ5: ≥20% AKV: ≥47 J | σs: ≥420 MPa σb: ≥500 MPa σ5: ≥22% AKV: ≥27 J (-18°C) | σs: ≥420 MPa σb: ≥500 MPa σ5: ≥22% | σs: ≥420 MPa σb: ≥500 MPa σ5: ≥22% AKV: ≥27 J (-29°C) | σs: ≥420 MPa σb: 500–660 MPa σ5: ≥22% AKV: ≥47 J (-20°C) |
| Shielding Gas Listed | CO2 | 80% Ar + 20% CO2 | CO2 | CO2 | CO2 |
| Applications | Low carbon steel and some low-alloy steel structures | Carbon steel and low-alloy steel structures | Carbon steel | Low carbon and high strength steel structures of 500MPa | Low carbon and high strength steel structures of 500MPa, high current welding |
Note: This table compares different welding wire grades and reproduces the original published values. The specifications of other grades do not describe the KYA 1.0mm ER70S-6 product. Select filler metal and welding procedures according to the application requirements and applicable technical standards.
KYA ER70S-6 solid MIG welding wire is intended for use with external shielding gas. Gas selection affects arc characteristics, metal transfer, weld bead appearance and spatter levels.
Pure carbon dioxide is commonly used for gas-shielded welding of carbon steel. It can provide good weld penetration under suitable welding conditions. Compared with many argon-rich gas mixtures, CO2 shielding may produce more spatter and different arc characteristics.
Argon-CO2 mixtures are also compatible with ER70S-6 wire. Depending on the gas composition and selected welding parameters, mixed gas can provide smoother arc behavior, improved bead appearance and reduced spatter compared with pure CO2.
The appropriate gas mixture should be selected according to the base metal, joint design, welding equipment and welding procedure requirements.
ER70S-6 solid welding wire is widely associated with industrial steel fabrication. Typical application areas for suitable welding procedures include:
Structural Steel Fabrication: Welding carbon steel structural components and fabricated assemblies.
Construction Machinery: Fabrication of frames, supports and steel components used in engineering equipment.
Shipbuilding: Selected carbon steel fabrication and assembly work where the filler metal meets the welding procedure requirements.
Bridge Fabrication: Welding suitable steel structural components under qualified procedures.
Coal Mining Machinery: Manufacturing and maintenance of steel machinery components.
Power Generation Equipment: Fabrication of applicable carbon steel structures and equipment.
Boilers and Pressure Vessels: Selected welding applications subject to applicable codes, approved procedures and material qualification.
Petrochemical Equipment: Fabrication of compatible carbon steel assemblies and supports.
High-Temperature Cyclone Separators: Selected steel fabrication work where service conditions and welding specifications permit ER70S-6 filler metal.
General Steel Manufacturing: Carbon steel fabrication using compatible gas-shielded welding equipment.
For critical structures, pressure-retaining equipment and elevated-temperature service, filler metal selection must satisfy the applicable welding procedure, design code and service requirements.
For welding consumable distributors, industrial suppliers and fabrication companies, consistent packaging specifications are important for purchasing, warehouse management and transportation planning.
The original KYA product information lists 5kg, 15kg and 20kg weight options. Its published bulk packing arrangement includes a 15kg/D270 plastic spool, 16kg per box, 72 boxes per pallet and 24 pallets per 20-foot general-purpose container.
The published payment terms are 30% T/T in advance and 70% balance against a copy of the bill of lading. The listed lead time is 10–25 days after receipt of deposit.
Buyers should confirm the required spool format, packing quantities, shipment configuration and current commercial terms with KYA before placing an order.
ER70S-6 1.0mm welding wire is a gas-shielded solid wire used primarily for joining carbon steel and selected low-alloy steel components. Common application areas include structural fabrication, machinery manufacturing, shipbuilding and general industrial steel welding.
Yes. KYA ER70S-6 solid welding wire is intended for welding with 100% CO2 or compatible argon-CO2 shielding gas mixtures. Welding parameters should be adjusted to the selected shielding gas and application.
ER70S-6 generally contains higher levels of manganese and silicon deoxidizers than ER70S-3. These elements help manage oxygen during welding and can improve tolerance of certain surface conditions. The appropriate grade should be selected according to the base metal, surface preparation and welding specifications.
ER70S-6 can be used in multiple welding positions, including flat, horizontal, vertical and overhead, provided the welding procedure and transfer mode are suitable. Welding position capability depends on the equipment settings, shielding gas and joint requirements.
The main difference is wire diameter. Wire size affects the available welding current range, deposition characteristics and suitable operating parameters. A 1.0mm wire and a 1.2mm wire require compatible drive rolls, contact tips and welding settings. Selection depends on base metal thickness, joint design and the required welding procedure.
Yes. ER70S-6 is a solid wire for gas metal arc welding and requires suitable external shielding gas. It is not a self-shielded flux-cored wire. The gas supply and welding environment must be appropriate to protect the weld pool.
The published KYA product information lists 5kg, 15kg and 20kg weight options. The detailed packing information specifies a 15kg/D270 plastic spool. Buyers should confirm the packaging configuration required for their order.
KYA's published packing details list 16kg per box, 72 boxes per pallet and 24 pallets per 20-foot general-purpose container for the specified packaging arrangement. Shipment quantities should be confirmed when preparing a commercial order.
Distributors and industrial buyers should specify the ER70S-6 classification, 1.0mm wire diameter, preferred spool weight, order quantity, destination and any applicable technical documentation requirements. This information helps KYA review the purchasing requirements.
ER70S-6 may be considered for certain pressure vessel welding applications when permitted by the applicable design code and qualified welding procedure. The filler metal classification alone does not establish suitability for every pressure vessel material or service condition.
KYA Fasteners supplies industrial fasteners and welding consumables for international customers. With more than 20 years of industry experience, KYA serves distributors, wholesalers and professional industrial buyers seeking welding wire and related fastening products.
For ER70S-6 solid MIG welding wire, customers can contact KYA to discuss product specifications, packaging requirements, order quantities and commercial arrangements.