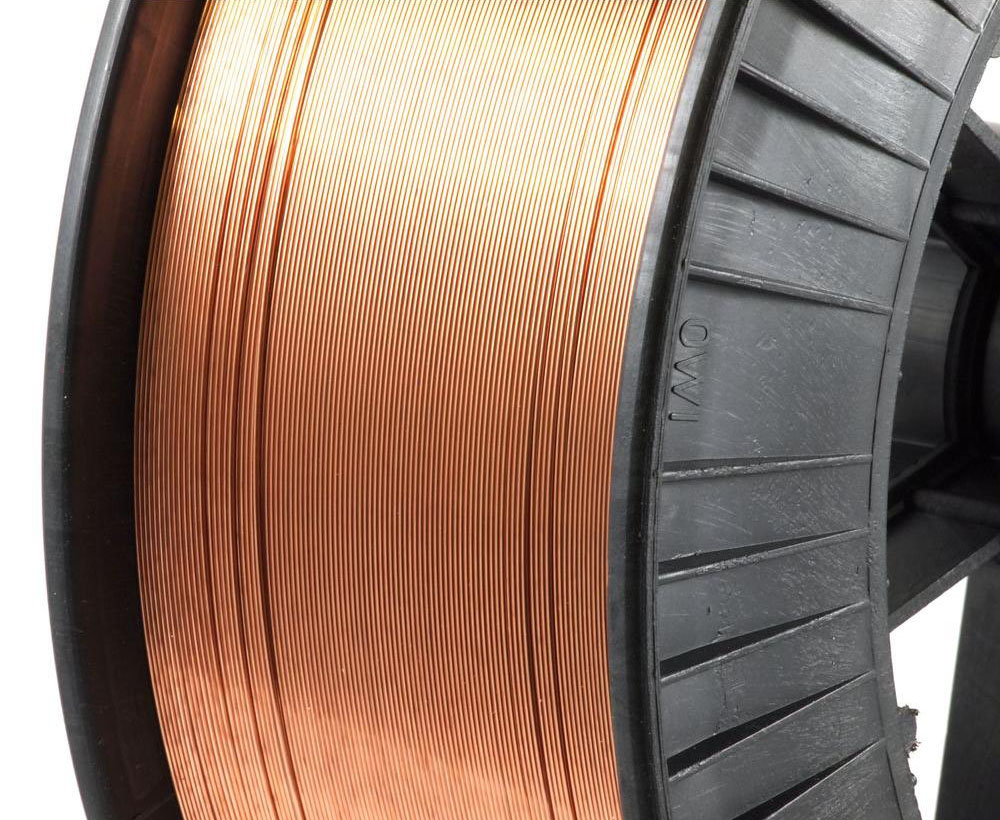
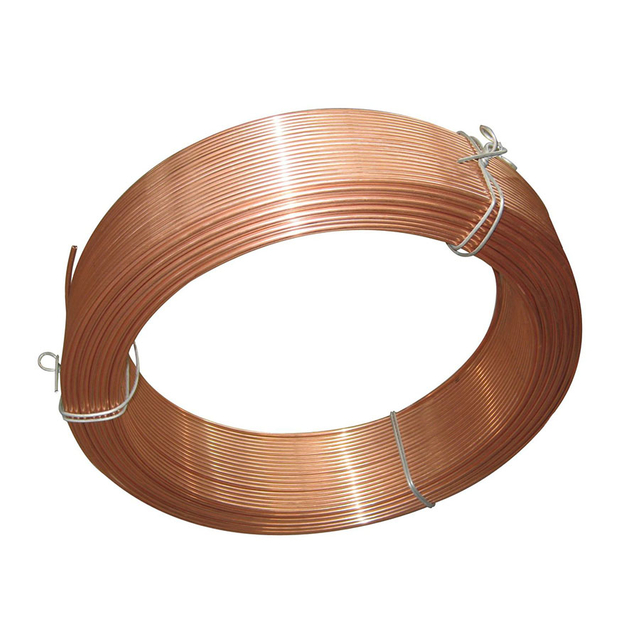
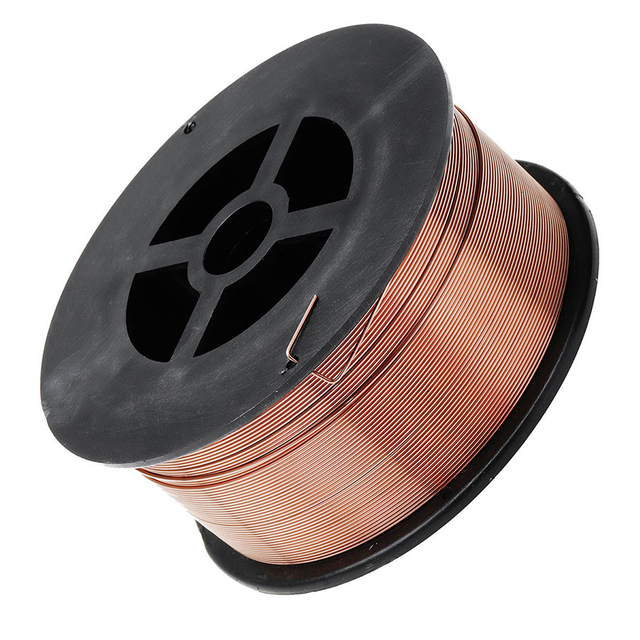
KYA ER70S-6 Mild Steel MIG Welding Wire is a copper-coated solid wire for gas metal arc welding (GMAW / MIG) of mild steel and suitable carbon-manganese steels. It is designed for use with 100% CO2 or Argon/CO2 mixed shielding gas in general fabrication, steel structures, machinery, automotive, shipbuilding and other industrial welding applications.
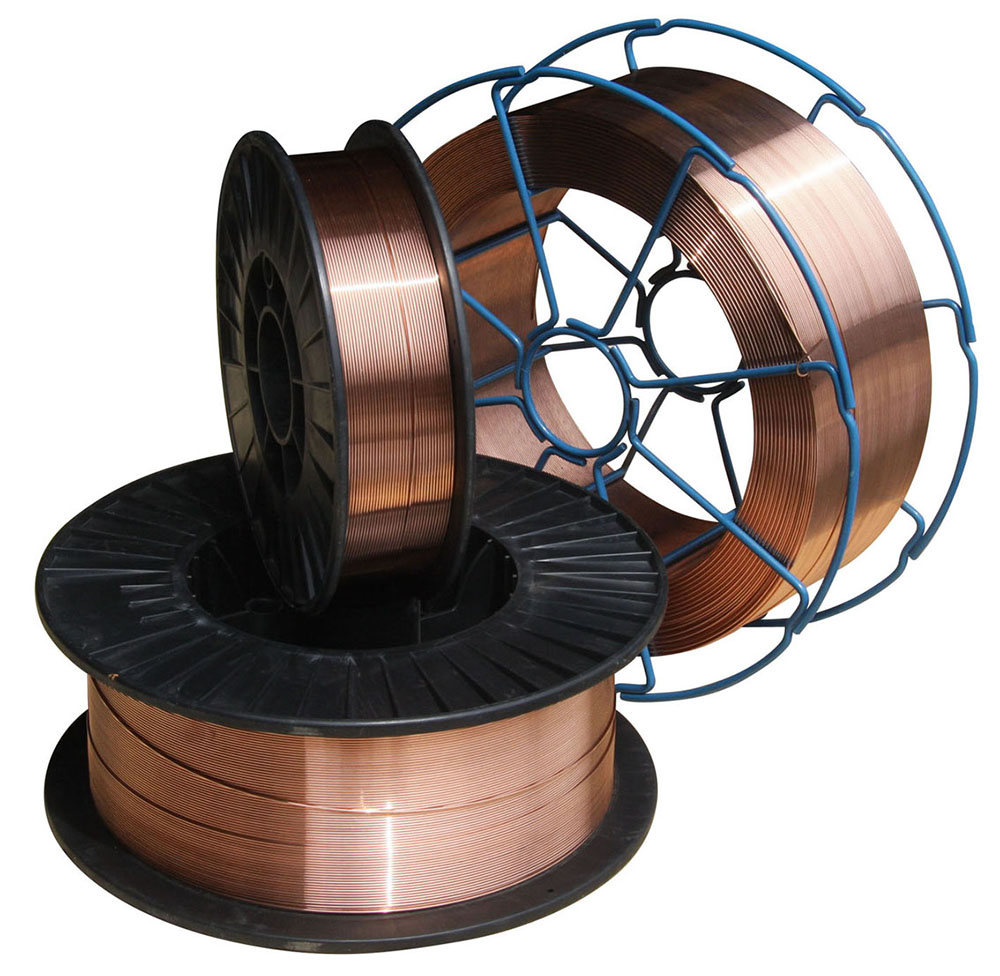
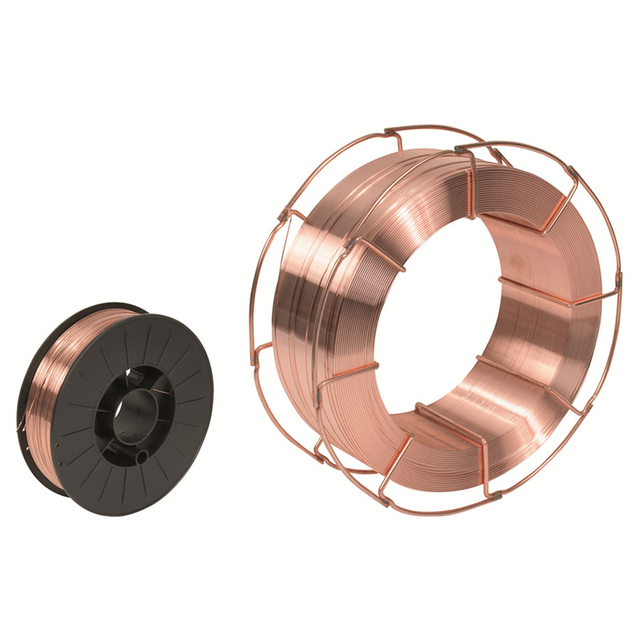
Available wire diameters include 0.8mm, 0.9mm, 1.0mm, 1.2mm and 1.6mm, with 5kg, 15kg and 20kg spool options. The product is listed as AWS A5.18 ER70S-6 / ER50-6.
ER70S-6 contains manganese and silicon deoxidizers that support stable welding performance on properly prepared mild steel and provide greater tolerance to light mill scale or surface oxidation than lower-deoxidizer solid wires. Base metal should still be cleaned according to the welding procedure whenever practical.
| Specification | Details |
|---|---|
| Product Type | Mild Steel Solid MIG / GMAW Welding Wire |
| AWS Classification | AWS A5.18 ER70S-6 |
| Related Grade | ER50-6 |
| Wire Type | Solid Wire |
| Base Alloy Type | Mild Steel / Carbon-Manganese Steel |
| Surface | Copper Coated |
| Available Diameters | 0.8mm, 0.9mm, 1.0mm, 1.2mm, 1.6mm |
| Spool Weight | 5kg, 15kg, 20kg |
| Spool Reference | D200 / D270 / D300 configurations depending on wire diameter and package; confirm exact spool before ordering |
| Welding Process | GMAW / MIG Welding |
| Shielding Gas | 100% CO2 or Argon / CO2 Mixed Gas |
| Polarity | DCEP is normally used for solid ER70S-6 GMAW; follow the welding procedure and equipment requirements |
| Typical Applications | General Fabrication, Steel Structures, Machinery, Automotive, Shipbuilding, Bridges, Pressure Vessels and Construction |
ER70S-6 is an AWS classification for carbon-steel solid welding wire. Understanding the designation helps welding distributors and fabricators select the correct filler metal.
| Designation | Meaning |
|---|---|
| ER | Electrode or rod filler metal |
| 70 | 70 ksi minimum tensile-strength classification under the applicable AWS specification |
| S | Solid wire |
| 6 | Identifies the ER70S-6 chemistry classification, including its manganese and silicon deoxidizer range |
| Grade | AWS Classification | Diameter | Package |
|---|---|---|---|
| ER50-6 | ER70S-6 | 0.8mm | 5 / 15 / 20kg per spool |
| ER50-6 | ER70S-6 | 0.9mm | 5 / 15 / 20kg per spool |
| ER50-6 | ER70S-6 | 1.0mm | 5 / 15 / 20kg per spool |
| ER50-6 | ER70S-6 | 1.2mm | 5 / 15 / 20kg per spool |
| ER50-6 | ER70S-6 | 1.6mm | 5 / 15 / 20kg per spool |
| ER50-G | ER70S-G | 1.0–1.6mm | 15 / 20kg per spool – related grade reference |
The correct wire diameter depends on base-metal thickness, transfer mode, welding current, deposition-rate requirement, joint design and welding equipment. Drive rolls, liner and contact tip should also match the selected wire diameter.
The following values are the typical chemical-composition data currently listed by KYA for this ER70S-6 product. For specification-controlled projects, request the applicable material certificate or batch test report before use.
| C | Mn | Si | P | S | Ni | Cr | Cu | V |
|---|---|---|---|---|---|---|---|---|
| 0.08% | 1.51% | 0.89% | 0.015% | 0.013% | 0.016% | 0.021% | 0.18% | 0.003% |
ER70S-6 uses manganese and silicon as important deoxidizing elements. These elements react with oxygen during welding and help reduce weld-metal porosity caused by limited amounts of surface oxidation or mill scale.
This higher deoxidizer level is one reason ER70S-6 is widely selected for general fabrication. It should not be interpreted as permission to weld through heavy rust, oil, paint or contamination; normal weld preparation remains important.
KYA currently lists the following representative deposited-metal properties under CO2 shielding gas. Actual test results depend on wire batch, shielding gas, welding procedure, heat input and test conditions.
| Tensile Strength | Yield Strength | Elongation | Impact Energy | Test Temperature | Shielding Gas |
|---|---|---|---|---|---|
| 545 MPa | 452 MPa | 29% | 91 J | -30°C | CO2 |
| Shielding Gas | General Welding Characteristics |
|---|---|
| 100% CO2 | Common economical shielding gas for ER70S-6; generally provides strong penetration but may produce more spatter than argon-rich mixtures depending on the welding parameters. |
| Ar / CO2 Mixed Gas | Argon-rich mixtures can provide a smoother arc, reduced spatter and different transfer characteristics depending on the exact gas ratio and welding parameters. |
KYA currently lists 100% CO2 and Argon with approximately 5–20% CO2 as applicable shielding-gas configurations. Gas selection should follow the required transfer mode, weld penetration, bead profile, spatter level and qualified welding procedure.
The following values are the parameter ranges currently listed by KYA. They should be used as starting references rather than fixed settings. Final current and voltage depend on base-metal thickness, joint design, wire feed speed, shielding gas, transfer mode, welding position and power source.
| Wire Diameter | Current Range | Voltage Range | Reference Current |
|---|---|---|---|
| 0.8mm | 50–120 A | 15–22 V | 100 A |
| 1.0mm | 70–180 A | 18–24 V | 150 A |
| 1.2mm | 80–350 A | 18–34 V | 280 A |
| 1.6mm | 140–500 A | 20–42 V | 350 A |
| Feature | ER70S-6 | ER70S-3 |
|---|---|---|
| Wire Type | Solid mild-steel MIG wire | Solid mild-steel MIG wire |
| Deoxidizer Level | Generally higher Mn / Si deoxidizer content | Generally lower deoxidizer content than ER70S-6 |
| Surface Condition | More tolerant of limited light mill scale or oxidation, although cleaning is still recommended | Typically preferred on cleaner base material |
| Typical Use | General fabrication, automotive, structural and industrial welding | General fabrication with appropriately prepared base material |
Copper coating supports consistent electrical contact between the wire and contact tip during GMAW operation.
A consistent wire surface and spool winding help support smooth feeding through the drive rolls, liner and contact tip. Feed performance also depends on correct feeder setup and consumable condition.
Consistent wire diameter, chemistry and feeding contribute to stable arc behavior when welding parameters and shielding gas are correctly selected.
ER70S-6 is widely used for welding mild-steel frames, fabricated components, brackets, assemblies and general industrial steelwork.
The wire can be used in structural fabrication where the filler-metal classification, base steel and qualified welding procedure meet the applicable project requirements.
Applications include automotive components, vehicle frames, trailers and other production environments requiring repeatable solid-wire MIG welding.
Engineering machinery, agricultural equipment and fabricated machine components are common applications for ER70S-6 solid welding wire.
ER70S-6 is used in shipbuilding and heavy fabrication where the applicable welding procedure, base material and project specification permit this filler-metal classification.
The classification can be used in selected pressure-vessel and piping fabrication, but code-controlled work should follow the qualified WPS, applicable construction code and required filler-metal certification.
| Diameter | General Selection Consideration |
|---|---|
| 0.8mm | Lower-current welding, thinner material and applications requiring finer heat-input control |
| 0.9mm | General light-to-medium fabrication and common MIG equipment configurations |
| 1.0mm | General fabrication requiring a balance of deposition rate and current range |
| 1.2mm | Medium-to-heavy fabrication and higher deposition requirements |
| 1.6mm | Higher-current industrial welding and heavier fabrication where equipment and procedure support the wire size |
| Purchasing Information | Information to Provide |
|---|---|
| Classification | ER70S-6 / ER50-6 |
| Wire Diameter | 0.8, 0.9, 1.0, 1.2 or 1.6mm |
| Spool Weight | 5kg, 15kg or 20kg |
| Spool Type | Confirm D200, D270, D300 or required feeder-compatible package |
| Shielding Gas | CO2 or required Ar/CO2 mixture |
| Application | General fabrication, structural steel, automotive, shipbuilding, machinery or other industrial welding |
| Required Documentation | Specify material certificate, batch test report or other documentation required for the project |
| Quantity | Spools, cartons, pallets or annual purchasing volume |
| Packaging | Standard packing or required private-label packaging |
ER70S-6 is a mild-steel solid MIG welding wire used for general fabrication, structural steel, automotive components, machinery, shipbuilding and many other carbon-steel welding applications.
ER70S-6 is classified as a mild-steel / carbon-manganese solid welding wire. It should not be described as #45 high-carbon steel.
ER70S-6 can be used with 100% CO2 or suitable Argon/CO2 mixed shielding gases. The gas mixture affects penetration, arc characteristics, transfer mode, bead profile and spatter level.
Yes. 100% CO2 is a commonly used shielding gas with ER70S-6 solid wire. Welding parameters should be adjusted for the selected wire diameter, transfer mode and joint.
Yes. Argon-rich CO2 mixtures are widely used with ER70S-6 and can provide smoother arc characteristics and reduced spatter compared with 100% CO2 under appropriate conditions.
ER70S-6 solid MIG wire is normally welded using DCEP, meaning direct current electrode positive. Always follow the wire specification, welding procedure and machine setup requirements.
ER70S-6 generally contains higher manganese and silicon deoxidizer levels, giving it greater tolerance to limited mill scale or surface oxidation. ER70S-3 is generally associated with cleaner steel surfaces. Proper base-metal preparation is recommended for both.
The KYA ER70S-6 product described on this page is copper coated. The coating supports electrical contact and consistent wire feeding when the welding system is correctly maintained.
The current KYA product range lists 0.8mm, 0.9mm, 1.0mm, 1.2mm and 1.6mm diameters.
KYA currently lists 5kg, 15kg and 20kg spool options. Confirm the exact spool diameter and hub configuration required by the wire feeder when ordering.
Its higher deoxidizer content provides more tolerance to limited mill scale or light surface oxidation than some lower-deoxidizer solid wires, but heavy rust, oil, paint and contamination should still be removed according to normal welding practice.
ER70S-6 can be used in multiple welding positions when the selected transfer mode, wire diameter, parameters and qualified procedure support that position. Welding-position capability should not be determined from the wire classification alone.
ER70S-6 is used in selected pressure-vessel fabrication, but code-controlled applications require the correct filler-metal documentation and a qualified welding procedure that meets the applicable construction standard.
Provide the required wire diameter, spool weight, spool type, shielding gas, application, quantity, required test documents, packaging and destination market.
Buyers requiring chemical or mechanical-property documentation should specify the required certificate or batch test report when requesting a quotation so availability can be confirmed for the order.
Ask About ER70S-6 Welding WireKYA supplies ER70S-6 mild-steel MIG welding wire for welding distributors, steel-structure factories, machinery manufacturers, automotive suppliers, shipyards, fabrication plants and other industrial users.
For quotations, provide the required ER70S-6 wire diameter, spool weight, spool configuration, shielding gas, quantity, documentation requirements and destination market.
Request a Bulk Quote