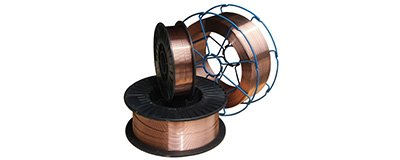
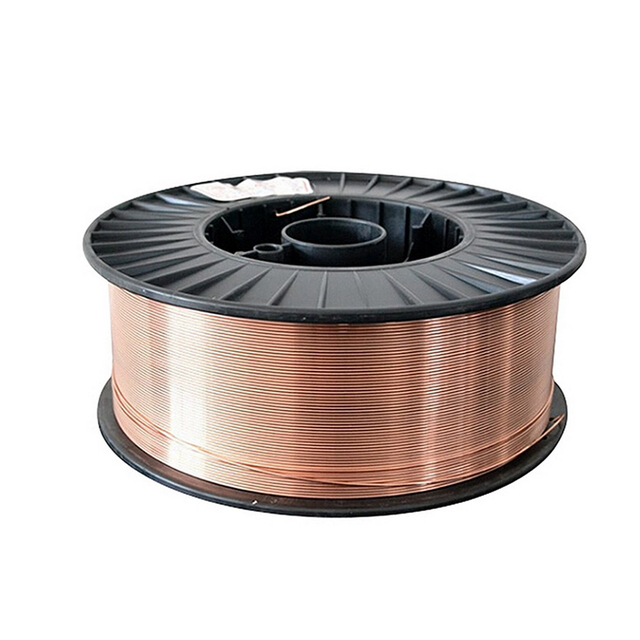
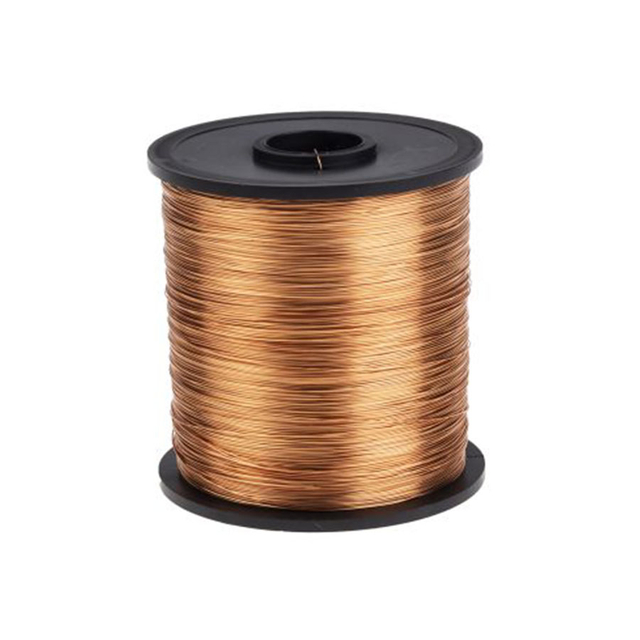
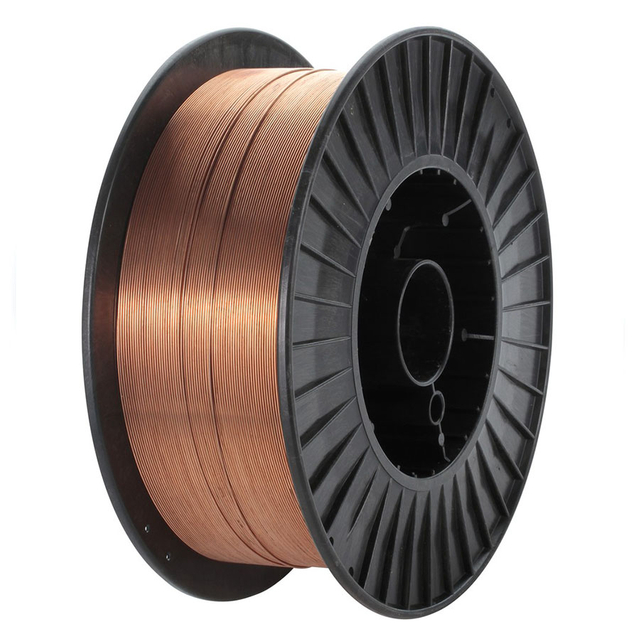
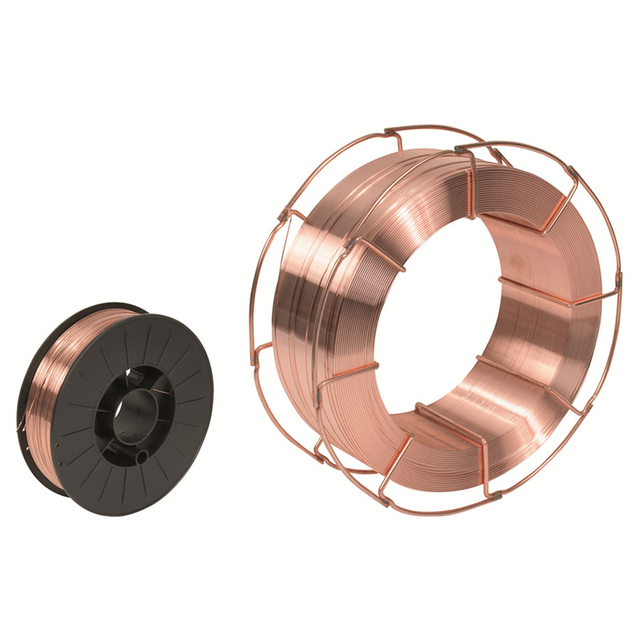
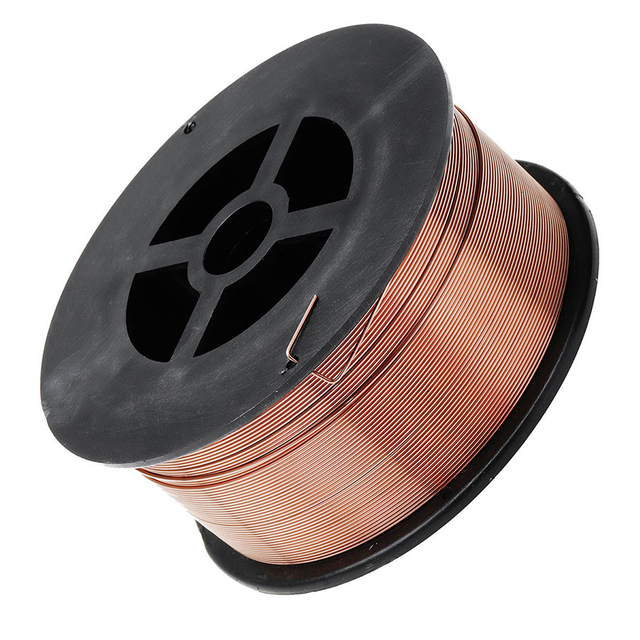
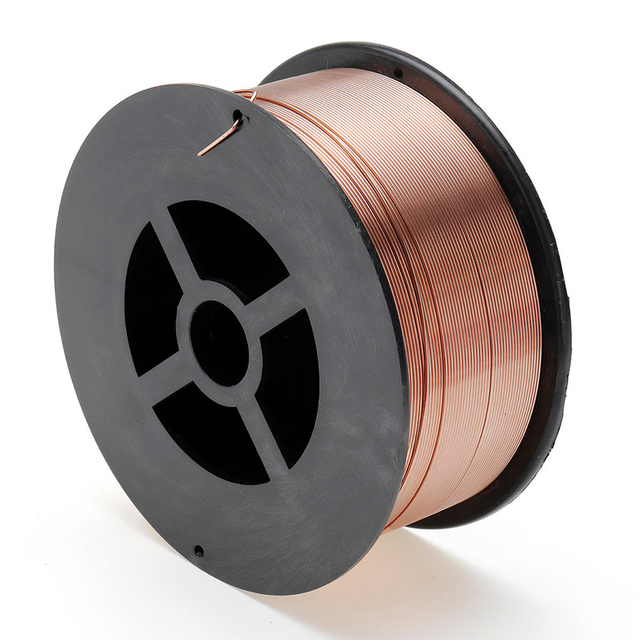
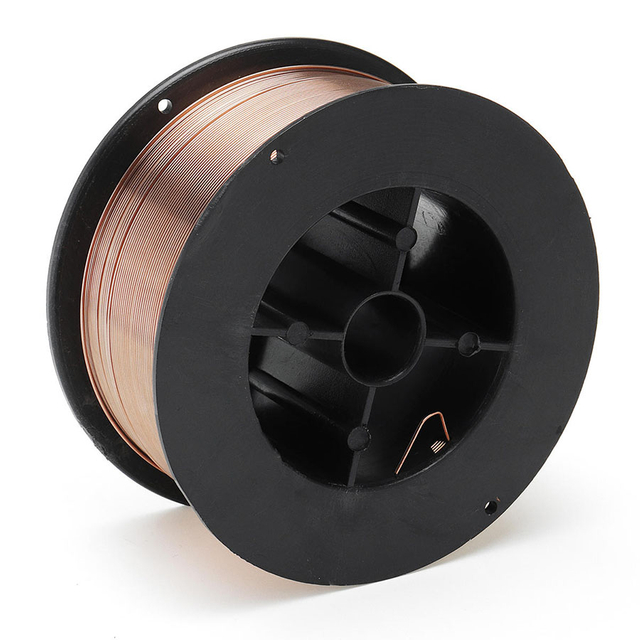
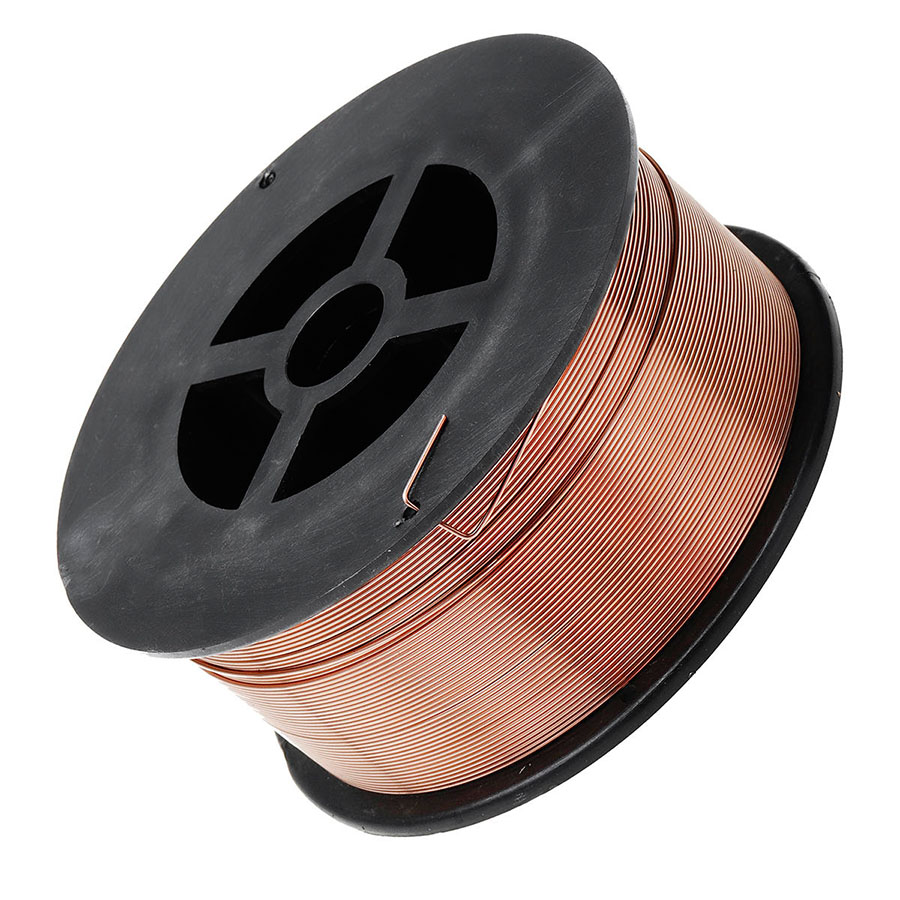
KYA ER70S-6 Copper Coated TIG Welding Wire is a carbon steel filler metal for welding mild steel and suitable carbon steel applications. Classified as AWS A5.18 ER70S-6, it contains relatively high levels of manganese and silicon deoxidizers and can be used for TIG/GTAW as well as MIG/GMAW when supplied in the appropriate product form and used with the correct welding procedure.
For conventional TIG welding of carbon steel, ER70S-6 filler metal is normally used with 100% argon shielding gas and DCEN polarity. Its manganese and silicon content supports weld puddle fluidity and helps provide useful tolerance to moderate surface oxidation and mill scale, although proper joint cleaning remains recommended for critical welding.
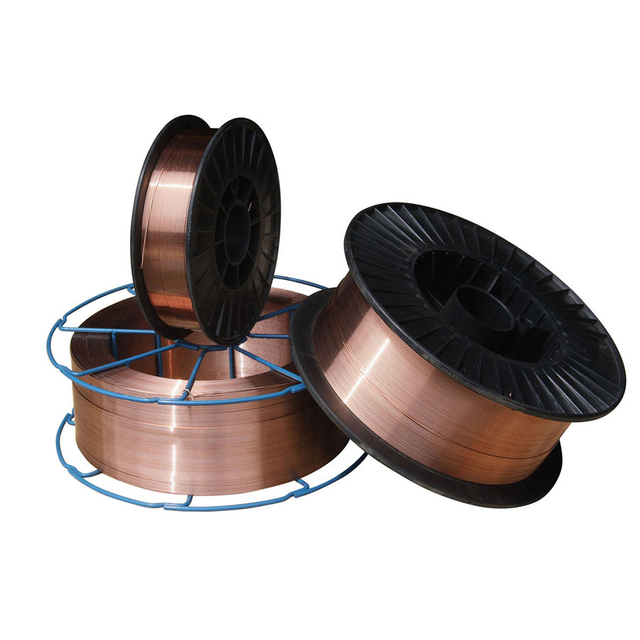
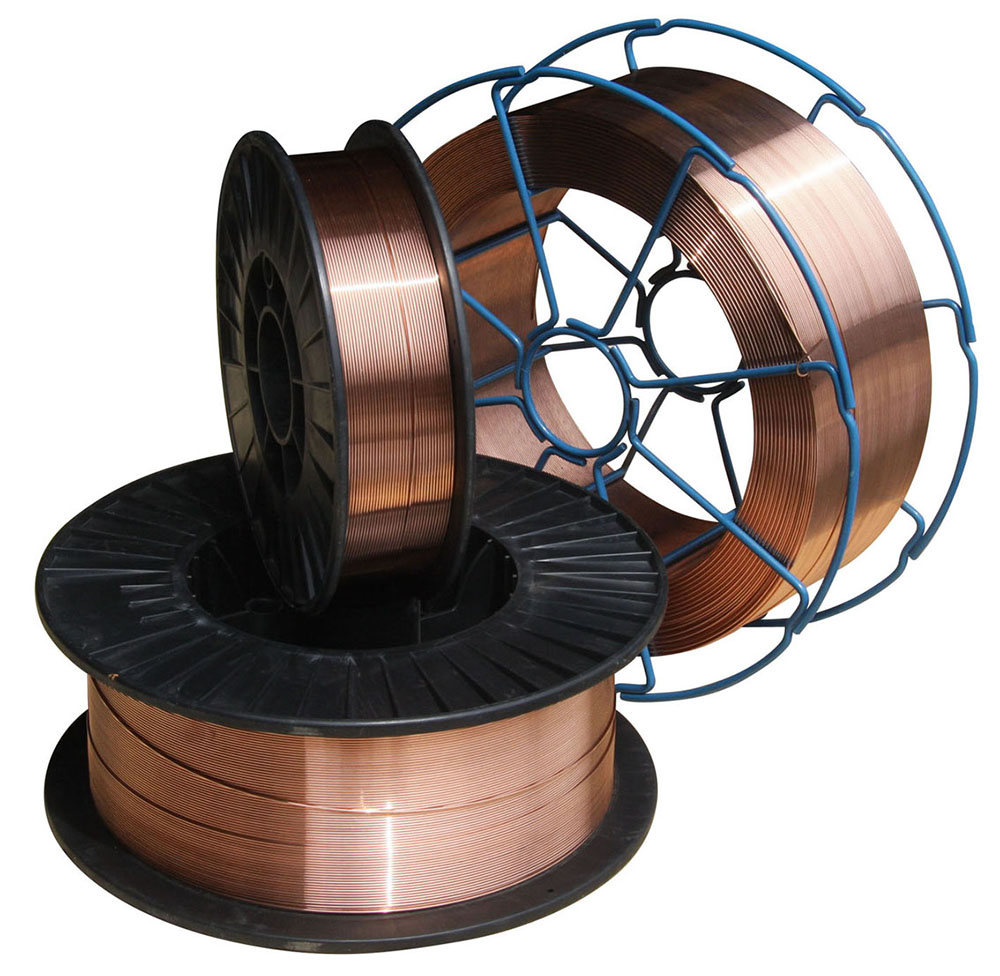
KYA lists diameters from 0.6mm to 1.6mm. The current KYA product data also lists 5kg, 15kg and 20kg spools plus 100-350kg drums. Buyers requiring conventional hand-fed TIG filler rods should confirm the required straight-cut rod form and packaging with KYA before ordering, while spool and drum packages are more commonly associated with continuous wire-feed welding applications.
 Request ER70S-6 TIG Wire Quote
| Specification | Details |
|---|---|
| AWS Classification | AWS A5.18 ER70S-6 |
| Referenced Designations | ER70S-6 / ER50-6 / SG2 / JIS YGW12; confirm applicable certification for the exact order |
| Filler Metal Type | Solid Carbon Steel Welding Wire / Filler Metal |
| Base Metal | Mild Steel and Suitable Carbon Steel |
| Surface | Copper Coated |
| Available Diameters | 0.6mm, 0.8mm, 0.9mm, 1.0mm, 1.2mm, 1.6mm |
| TIG / GTAW Shielding Gas | 100% Argon |
| Typical TIG Polarity | DCEN / Direct Current Electrode Negative |
| MIG / GMAW Shielding Gas | 100% CO2, Ar + 5% CO2, Ar + 2% O2 as listed in KYA product data |
| Listed Spool Packaging | 5kg, 15kg, 20kg |
| Listed Drum Packaging | 100-350kg |
| Spool Types | D270, D300 Plastic Spool; K300 Metal Spool |
| Manual TIG Rod Form | Confirm cut-length rod diameter, length and package with KYA before ordering |
ER70S-6 can be used as a carbon steel filler metal in both TIG/GTAW and MIG/GMAW, but the shielding gas, polarity, filler delivery method, packaging and welding parameters are different. These processes should not be presented as interchangeable.
| Item | TIG / GTAW | MIG / GMAW |
|---|---|---|
| Filler Classification | ER70S-6 | ER70S-6 |
| Typical Filler Form | Straight cut-length filler rod or compatible automated wire feed | Continuous wire on spool or drum |
| Shielding Gas | 100% Argon | CO2 or suitable argon-based gas mixture |
| Typical Steel Polarity | DCEN | Typically DCEP |
| Filler Delivery | Filler is introduced separately into the weld pool | Wire electrode is continuously fed through the welding gun |
| Typical Purchasing Form | Rod tube / box for manual TIG | Spool or bulk drum |
If your application is conventional manual TIG welding, tell KYA the required filler diameter, cut length, package weight, base metal and welding procedure. If you need continuous wire on a D270, D300 or K300 spool, specify whether the application is MIG/GMAW or an automated wire-fed TIG process.
ER70S-6 is characterized by relatively high manganese and silicon content compared with some other carbon steel filler metals. These deoxidizers support weld pool behavior and provide useful tolerance to moderate levels of mill scale and surface oxidation.
| Element | ER70S-6 Range / Maximum |
|---|---|
| Carbon (C) | 0.06-0.15% |
| Manganese (Mn) | 1.40-1.85% |
| Silicon (Si) | 0.80-1.15% |
| Phosphorus (P) | ≤0.025% |
| Sulfur (S) | ≤0.035% |
| Copper (Cu) | ≤0.50% |
Buyers requiring certified chemistry should request the applicable material certificate or batch test data for the exact product supplied rather than relying only on nominal classification limits.
The following mechanical property values are retained from the current KYA product data. Actual deposited weld-metal properties depend on welding process, shielding gas, heat input, joint design, base material and test conditions.
| Test Item | KYA Guarantee Value | Listed General Result |
|---|---|---|
| Tensile Strength | ≥500 MPa | 558 MPa |
| Yield Strength | ≥420 MPa | 472 MPa |
| Elongation | ≥22% | 27% |
| Impact Energy at -30°C | ≥27 J | 98 J |
For TIG/GTAW welding of mild and carbon steel, ER70S-6 should normally be used with 100% argon shielding gas and DCEN polarity. TIG amperage should be selected according to base-metal thickness, filler rod diameter, tungsten diameter, joint design, welding position and qualified welding procedure.
| TIG Parameter | Recommended Approach |
|---|---|
| Process | GTAW / TIG |
| Shielding Gas | 100% Argon |
| Polarity | DCEN for typical carbon steel TIG welding |
| Filler Diameter | Select according to base-metal thickness, joint size and required deposition |
| Surface Preparation | Remove excessive rust, oil, moisture, paint and contamination before critical welding |
| Amperage | Determine from material thickness, tungsten size, filler size, joint design and approved WPS |
Do not use the CO2 gas-flow values in the following section as TIG parameters. They belong to the continuous-wire MIG/GMAW reference data currently supplied with this KYA product.
The current KYA source page also supplies the following welding-current and CO2-flow data. Because these values use CO2 shielding gas, they should be identified as MIG/GMAW reference parameters, not TIG welding parameters.
| Wire Size | Welding Current | CO2 Flow Rate |
|---|---|---|
| 0.6mm | 50-80 A | 10-15 L/min |
| 0.8mm | 50-100 A | 15 L/min |
| 1.0mm | 50-220 A | 15-20 L/min |
| 1.2mm | 80-350 A | 15-25 L/min |
| 1.6mm | 170-550 A | 20-25 L/min |
These are KYA reference values for continuous-wire gas-shielded welding. Actual MIG/GMAW settings depend on shielding gas, transfer mode, base-metal thickness, wire-feed speed, contact-tip-to-work distance and the applicable welding procedure.
AWS A5.18 ER70S-6 Classification: Carbon steel filler metal widely used for welding mild and suitable carbon steels.
High Mn and Si Deoxidizer Content: Supports puddle fluidity and provides useful tolerance to moderate mill scale and surface oxidation.
Copper-Coated Surface: Provides the specified surface finish and helps protect the filler wire surface during normal handling and storage.
Suitable for TIG/GTAW: Use 100% argon and appropriate DCEN welding parameters for conventional carbon steel TIG applications.
Multiple Diameters: Available KYA sizes range from 0.6mm to 1.6mm for different welding and wire-feed requirements.
Good Weld Pool Fluidity: The silicon level associated with ER70S-6 supports wetting and smooth bead formation when suitable welding procedures are used.
Industrial Carbon Steel Applications: Suitable for fabrication, machinery, construction, shipbuilding and related carbon steel welding where ER70S-6 is specified.
ER70S-6 is used for welding mild steel and suitable carbon steel components where good puddle control, wetting behavior and deoxidizing capability are required. For TIG/GTAW, it can be used as filler metal in manual or automated welding processes according to the joint design and qualified welding procedure.
| Application | Typical Use |
|---|---|
| Steel Structures | Suitable carbon steel fabrication where ER70S-6 is permitted by the welding procedure. |
| Engineering Machinery | Welding frames, brackets, machinery components and fabricated assemblies. |
| Shipbuilding | Selected carbon steel marine fabrication subject to approved welding procedures. |
| Bridges | Structural carbon steel welding where the specified filler metal and WPS permit ER70S-6. |
| Pressure Vessels | Welding applications subject to the applicable material, code and procedure requirements. |
| Construction | General carbon steel fabrication and repair. |
| Petrochemical Equipment | Selected carbon steel fabrication according to engineering requirements. |
| Boilers & Power Equipment | Applications where the required welding specification permits ER70S-6 filler metal. |
Filler diameter should be selected according to base-metal thickness, joint geometry, required deposition rate, welding position, heat input and welding process. The smallest or largest available diameter is not automatically the best option.
| Diameter | Selection Consideration |
|---|---|
| 0.6-0.8mm | Small-diameter filler for applications requiring relatively fine heat and filler control; confirm TIG product form. |
| 0.9-1.0mm | Intermediate filler sizes for suitable light and general fabrication. |
| 1.2mm | Larger filler or continuous-wire size for higher deposition requirements with suitable welding equipment. |
| 1.6mm | Larger filler size for suitable thicker joints or higher deposition applications. |
ER70S-6 and ER70S-2 are both carbon steel filler classifications used in TIG welding, but their deoxidizer systems differ. The correct filler should follow the base material, welding procedure and project requirements rather than assuming the two grades are always interchangeable.
| Feature | ER70S-6 | ER70S-2 |
|---|---|---|
| Material Family | Carbon steel filler metal | Carbon steel filler metal |
| Primary Deoxidizers | Relatively high manganese and silicon | Different multi-element deoxidizer system |
| Selection | Follow the applicable WPS, engineering requirement and base-metal specification. | |
KYA supplies ER70S-6 welding filler metal for welding distributors, industrial supply companies, steel fabricators, machinery manufacturers, construction companies, shipyards and other professional buyers.
Because TIG rod and MIG wire use different product forms and packaging, buyers should clearly specify the welding process when requesting a quotation. For TIG applications, provide the required filler diameter, straight rod length if applicable, package weight, base metal and required standard. For continuous wire applications, provide spool or drum type and welding process.
Buyers requiring AWS certificates, chemical analysis, mechanical test data or other inspection documents should include those requirements with the inquiry so the exact product specification can be confirmed before production.
Request Wholesale Price Explore Welding Wire
Yes. ER70S-6 can be used as a carbon steel filler metal for TIG/GTAW when supplied in an appropriate filler form and used with the correct shielding gas and welding procedure.
Conventional TIG/GTAW welding of carbon steel with ER70S-6 normally uses 100% argon shielding gas.
No. CO2 and argon/CO2 mixtures are associated with MIG/GMAW applications. Conventional TIG welding with ER70S-6 should use an inert shielding gas such as 100% argon.
DCEN, or direct current electrode negative, is typically used for TIG welding of mild and carbon steel.
ER70S-6 is a carbon steel electrode and rod classification covered by AWS A5.18.
ER70S-6 is primarily used for suitable mild and carbon steels. It should not automatically be used for stainless steel, aluminum or other alloy systems requiring different filler-metal classifications.
Manganese and silicon act as deoxidizers and support weld puddle behavior. This gives ER70S-6 useful tolerance to moderate mill scale and surface oxidation compared with lower-deoxidizer carbon steel fillers.
ER70S-6 should not be described as a low-hydrogen electrode classification in the same sense as low-hydrogen SMAW electrodes such as E7018. Filler material should still be stored clean and dry and protected from oil, moisture and contamination.
The filler-metal classification can be the same, but product form and welding method differ. Manual TIG normally uses straight filler rods, while MIG uses continuously fed wire supplied on a spool or drum.
Continuous spool wire can be used in specialized automated or mechanized TIG wire-feed systems, but conventional manual TIG normally uses straight cut-length filler rods. Confirm the welding process and required product form before ordering.
The current KYA product data lists 0.6mm, 0.8mm, 0.9mm, 1.0mm, 1.2mm and 1.6mm diameters. Confirm availability in the required TIG rod or continuous wire form.
The current KYA product data lists a guarantee value of at least 500 MPa and a general result of 558 MPa. Actual weld-metal performance depends on process and test conditions.
Its relatively high manganese and silicon content provides useful tolerance to moderate surface oxidation and mill scale. Critical welding should still follow the required cleaning procedure and WPS.
The current KYA product data lists 5kg, 15kg and 20kg spools plus 100-350kg drums. Buyers requiring conventional TIG filler rods should separately confirm straight rod length and packaging availability.
Store it in a clean and dry environment and protect the filler metal from moisture, oil, dust, rust and other contamination before welding.
Yes. Welding distributors, steel fabricators, machinery manufacturers and other industrial buyers can contact KYA for diameter, packaging, certification and bulk purchasing requirements.
Looking for ER70S-6 copper coated TIG welding filler metal? Send KYA Fasteners your welding process, filler diameter, required product form, package weight, base-metal specification, purchase quantity, destination country and certification requirements. For TIG applications, specify whether you require straight filler rods or continuous wire for an automated TIG system.